

UV Printing vs Pad Printing and Offset: Decorating Curved and Flat Parts
- by Andresjet
Print bigger, print faster — wide-format UV flatbed printers for signs, decor and industrial work.

Pad printing and direct UV printing are often compared as though one were replacing the other, yet they solve different problems. Pad printing reaches small curved parts that cannot be laid flat, using a shaped pad that presses ink onto the surface. Direct UV printing applies ink without contact to items that can be held and rotated or placed on a bed. The decision follows geometry, artwork and order pattern rather than technology preference.
This guide sets out how the two processes differ physically, which parts belong to each, how artwork complexity and version count change the answer, and how to qualify a small curved part before committing a decoration programme to either route.
One presses; the other deposits without contact.
Pad printing transfers ink from an etched plate using a shaped silicone pad that presses against the part, while direct UV printing deposits ink from a print head and cures it with ultraviolet energy.
The contact difference has consequences that reach beyond the printing step. Because the pad presses against the part, the part has to be supported during the stroke, the pad has to be shaped to the geometry, and the deformation of the pad is what allows ink to follow a curve. That is why pad printing excels on small, rigid, curved items with a defined printable face — a closure, a cap, a small component — and why the artwork is normally a set of flat spot colours that the pad can transfer without distortion.
Direct printing has no pad, so the constraints move elsewhere. The part has to be held and positioned by a fixture or by vacuum, and on the cylinder route it is rotated while the print head lays ink around the circumference. Nothing has to be produced before printing begins, which changes the economics of short and variable runs entirely.
Small, rigid, curved parts with a stable spot-colour design.
Where the printable face is limited, the design is a few flat colours and the item repeats, a contact process can be efficient and straightforward.
The parts that fit this description share four properties. They are small enough for the pad to cover the print area in one stroke. They are rigid enough to be supported without deforming. They have a defined surface that the pad can reach without interference from adjacent features. And their artwork is stable, because the setup belongs to the design — a new design is a new setup, and each additional colour is an additional registration step.
The limitation is coverage. A pad transfers a face, not a continuous wrap, so a design that needs to run all the way around a cylinder or across a shoulder is not a natural pad-printing job. Where a customer asks for a 360-degree graphic on a tapered vessel, the geometry itself points to a rotating platform rather than to a pressed face.
Items within the published geometry range, with no setup.
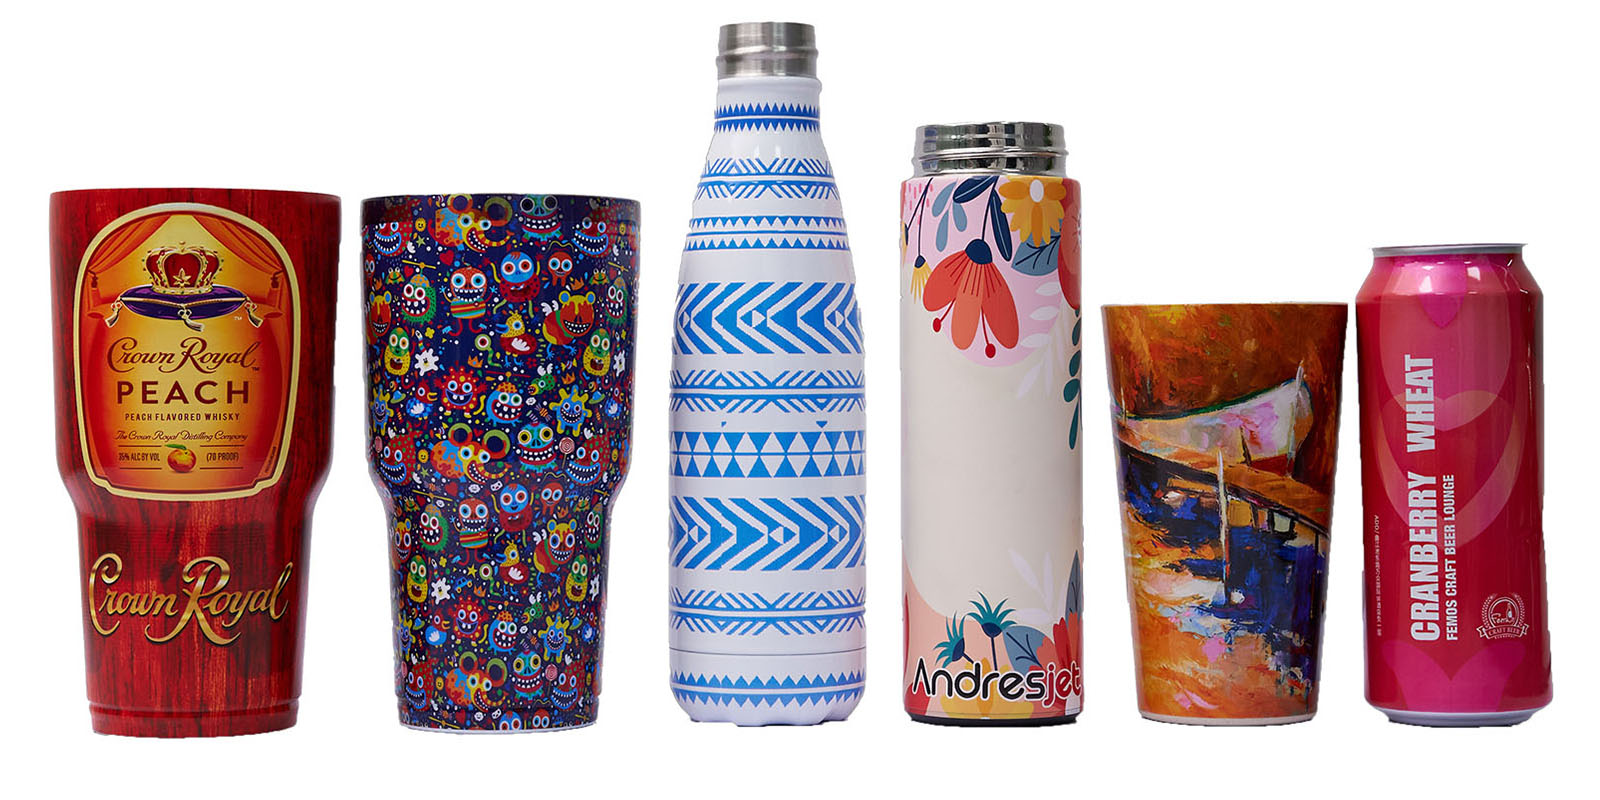
Direct printing handles rigid and pre-formed items, with a separate cylinder route for bottles, cups and tapered containers.
The published cylinder route accepts a standard part diameter range of 60 to 170 mm, optional ranges of 10 to 60 mm and 170 to 240 mm, a taper angle range of 0 to 7 degrees and a print length of 40 to 270 mm, with an object weight up to 3 kg. Ink is published as K, C, M, Y, white and varnish, with print modes of stepping or helix. On the flat route, the same range includes compact platforms for small nested parts and large beds for panels, so a workshop can decorate a cap-and-container assembly on two machines rather than outsourcing one of them.
The commercial advantage is not print quality but the absence of setup. Where the design changes, the version count is high, or the run is short, the cost structure of direct printing is fundamentally different from a process that has to produce a plate for each design. That difference is what the published comparison guidance calls out when it notes that direct printing suits full-colour artwork, personalisation and short-to-medium runs, while established plate or screen processes may suit stable repeat designs.
More colours and detail push towards digital.
Each colour in a plate-based contact process adds a plate and a registration step, while a digital press handles additional colours as part of the same file.
This is the variable that most often settles a real comparison, because it changes the setup cost rather than the running cost. A one-colour logo on a closure is a natural contact-printing job. The same logo with a gradient and a photographic element is a digital job, because reproducing it by pressing would require multiple plates and careful registration on a curved surface. Where a brand's guideline includes a specific colour that must be matched, opacity and coverage also differ between a pressed film and a printed layer, and that difference should be judged on the actual part.
The published direct-printing guidance places the emphasis on testing rather than on assertion: multi-colour work with white and varnish layers is supported as separate digital layers, but the appearance has to be approved on the production item under the viewing condition it will be seen in. The same discipline applies on the other side of the comparison, which is why a comparison run on the customer's actual part is more useful than a comparison run on a sample supplied by either process.

Digital absorbs versions cheaply; contact printing does not.
Where an order carries many designs or personalised data, the setup attached to each version is the largest cost difference between the routes.
Consider a promotional order of two hundred closures across eight designs, two of which are personalised. On a contact process that is eight or more setups, each with its own plate and registration, before any production. On a direct-printing route it is eight files and one fixture, which is why the published material for this range describes personalisation and mixed-version work as a normal digital workload rather than a special case.
Where the order pattern reverses — a single design in high volume with no changes — the advantage moves back towards the contact process, because the setup is amortised across a large quantity. The decision rule is therefore about version count and change frequency, not about the size of any individual order.
One changes tooling; the other changes the fixture and file.
Changeover is where the two routes differ most in operational terms, and it is also where a production plan can be lost if it is not measured.
On the direct-printing cylinder route, a changeover can require the correct fixture or an adjustment to it, artwork resized to the new circumference, height and focus checks, rotation calibration and a sample print. The published description of changeover notes that the time depends on how different the products are and whether a dedicated fixture is already available — which is why fixture strategy is a capacity decision rather than a tooling detail. A workshop running the same container family repeatedly should hold the fixtures for it; a workshop running mixed promotional work should budget for fixture changes as a recurring production step.
On a contact process, changeover is dominated by the plate and the pad setup for each design. That makes the two routes complementary in a mixed workshop: plate-based work for stable designs and long repeats, digital work for short runs, versions and personalisation. Decorating curved parts by printing rather than pressing is an engineering capability of the cylinder route rather than a claim about the process being superior.
Adhesion, rub resistance and the finished assembly.
Testing should use the production part, the intended artwork and the conditions the finished product will meet, because the geometry of a small curved part makes it a different test from a flat panel.
Adhesion is assessed with the tape method under ASTM D3359 (ASTM D3359) and resistance to handling and cleaning under ASTM D4060 (ASTM D4060). On closures and caps, the test that matters most is often the assembly one: the decorated part should be fitted, torqued, opened or washed as it will be in service, because the stress at a thread or a snap feature is where a decoration fails rather than on the flat area between features.
Where the part will be exposed to moisture or cleaning chemicals, resistance under ASTM D2247 is the relevant additional test (ASTM D2247). Colour consistency across a repeat programme depends on the profiles maintained for that part surface (International Color Consortium), and process control practice for industrial print environments is covered by certification and research bodies in the field (Fogra). The wider trade guidance on process selection is a useful reference when the comparison between two viable routes is close (PRINTING United Alliance).
Yes, and allocation is the point.
Many decorators run digital and contact processes side by side and allocate work by quantity, colour count and version count.
The allocation rule is straightforward once the numbers are known: long repeats of a simple spot-colour design go to the contact process, while short runs, multi-colour artwork, personalisation and any job with several versions go to direct printing. What makes the rule work in practice is measuring the setup on both sides, because a shop that has never timed a plate change on a curved part tends to overestimate how cheap the contact route is on small quantities.
Where the two routes produce the same product for the same customer, colour consistency between them becomes a specification item in its own right. Holding a shared physical reference and the profiles for the substrate keeps the two outputs close enough to be used together in one range.
By quantity, colour count and version count.
Those three variables account for most of the difference between a pressed face and a printed wrap, and they can be answered from the order book rather than from a technology comparison.
| Order characteristic | Favours contact printing | Favours direct UV printing |
|---|---|---|
| Quantity per design | High, with the setup amortised | Low to medium |
| Colour count | One to three flat spot colours | Multi-colour, gradients, photographic detail |
| Versions per order | One or two stable designs | Many versions, or personalised data |
| Coverage required | A defined face on a small curved part | A continuous wrap around a cylinder or taper |
| White or varnish layers | Handled within the plate design | Printed as separate digital layers |
What is the physical difference between pad printing and direct UV printing?
Pad printing transfers ink from an etched plate by a shaped silicone pad that presses against the part. Direct UV printing deposits ink from a print head and cures it with ultraviolet energy without contact. That difference decides which geometries and artwork any given part can accept.
Which parts suit pad printing?
Small parts with a defined printable face where a single or few spot colours are required and the design repeats. It is a contact process, so geometry, wall rigidity and support during the press stroke all matter, and setup is tied to producing a plate for each design.
Which parts suit direct UV printing?
Rigid and pre-formed items within the published media and geometry ranges, including cylindrical and tapered containers through the cylinder route. Nothing has to be produced before printing, so artwork changes and mixed versions cost almost nothing to absorb.
How does artwork complexity change the decision?
Multi-colour images, gradients and photographic detail are natural for digital printing and progressively harder for a plate-based contact process, where each colour adds a plate and a registration step. Where the design is a single flat spot colour, that difference disappears.
Can both processes coexist in one workshop?
Yes, and many decorators run both, allocating work by quantity, colour count and version count. The two routes are complementary rather than exclusive, and the allocation should follow the order pattern rather than a general preference for one technology.
Pad printing and direct UV printing reach different parts. A contact process suits small, rigid items with a defined face and a stable spot-colour design; direct printing suits items that can be held and rotated, multi-colour artwork, and orders with many versions. Where the two overlap, quantity, colour count and version count decide it.
Run the comparison on the customer's actual part and include the setup and assembly test on both sides, because the difference is usually in the setup rather than in the printing. The published cylinder range and container routes are set out in the UV printers for bottles and tumblers and cosmetic bottle and tube collections, with small-part routes covered under medals, coins and buttons.
Send the part, the artwork and the order pattern. We will confirm whether the published cylinder or flat route suits it, and return printed samples with the fixture and settings recorded.
Request part sample testing


