

- by John White
Flatbed vs Cylinder UV: Choosing for a Mixed Promo and Panel Order Book
- by John White
Curved surfaces? Print straight onto bottles, tubes and cylinders — no labels needed.
This guide is for print shops routing a mixed order book that includes rigid panels, flat promotional products, drinkware, and other cylindrical parts. It helps production managers decide whether one platform can cover the work or whether separate flatbed and cylinder capacity protects scheduling. Shops printing only flexible rolls should skip it.
Last updated:
The central issue is not whether both machine types can place UV ink on an object. It is whether the shop can hold each object consistently, reach the required print area, maintain registration, and move from job to job without consuming too much operator time. A flat sign panel and a tapered tumbler impose different mechanical demands even when their artwork uses the same colors.
Buyers comparing a flatbed vs cylinder UV printer usually need a routing decision, not a feature contest. They must identify which orders require a stationary flat work surface, which require controlled rotation, and how often the production team would interrupt flat work to install, align, test, and remove a rotary fixture.
A useful order-book review separates work into three lanes:
Flatbeds typically win the first two lanes because their printable bed supports boards and lets operators gang many small pieces. Dedicated cylinder machines are built around the third lane, where synchronized rotation creates a continuous wrap and taper compensation may be essential. A flatbed with a rotary attachment can bridge occasional round jobs, but the attachment does not remove setup and scheduling friction.
Shortlisting should begin with part geometry, required image coverage, batch pattern, and available production hours. Treat bed size, accepted diameter, part length, weight, ink configuration, fixture access, and taper capability as gates. A model that misses one compulsory dimension or finish should not advance merely because other specifications look attractive.
Use a representative SKU list rather than a single easy sample. For every item, record the printable area, overall dimensions, material and coating, surface color, expected white or varnish use, quantity pattern, wrap angle, and acceptable seam location. Note whether the artwork crosses a handle or must stop before a rim. These details determine both machine access and fixture design.
| Order-book question | Flatbed implication | Dedicated cylinder implication |
|---|---|---|
| Are large rigid boards routine? | Bed area and loading access are primary | Not a suitable panel route |
| Are many small flat blanks repeated? | A multi-up nest can reduce handling | Rotation adds no advantage |
| Are full wraps on drinkware routine? | Rotary setup may interrupt flat production | Continuous round work fits the platform |
| Are tapered parts common? | Confirm attachment capability and sample result | Confirm taper range and compensation workflow |
| Do flat and round deadlines overlap? | One shared platform creates a scheduling conflict | Separate queues may preserve capacity |
Non-negotiables should be written into the sample request. Specify measurable artwork placement, seam tolerance, color target, adhesion test, visible banding limits, surface defects, and the acceptance method. This makes competing demonstrations comparable without inventing a universal reject rate.
AndresJet offers distinct starting points for round, compact flat, and wide-format rigid work. The right mapping depends on verified part dimensions and samples, not model names alone. Review every specification on the linked product page, then ask the supplier to confirm configuration, options, throughput assumptions, and fixture scope on a written quote.


For routine cylindrical production, the AJ360i digital cylinder printer is presented for parts 60-170 mm in diameter, up to 270 mm long, and up to 3 kg. Its listed ink set is CMYK plus white and varnish. Marketing throughput is up to approximately 60 items per hour in production mode or approximately 40 in high-quality mode. Those figures depend on image, passes, surface, and workflow, so verify them with representative files and products. The broader digital cylinder printer collection provides the category context.
For compact rigid work, the AJ1206 small UV flatbed printer lists a 1200 x 600 mm area, 0-35 mm material thickness, CMYK plus white and varnish, and optional CCD positioning. It is a candidate for panels within that envelope and nested promotional blanks.
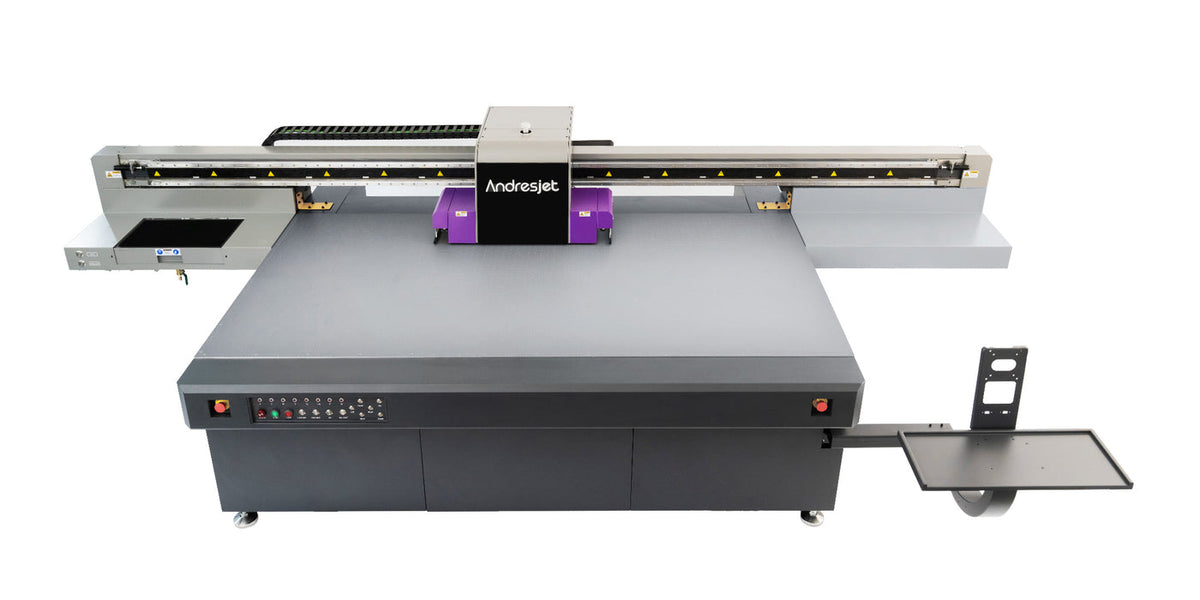
For larger boards or higher-area demand, the AJ3220G/R UV flatbed printer lists a 3200 x 2000 mm format, four to eight Ricoh heads, CMYK plus white and varnish expandable to eight colors, and dual negative pressure. Its marketing figure is approximately 35.88 square meters per hour for four-color production. The wide-format UV flatbed printer collection spans listed areas from 2100 x 3000 to 3200 x 2000 mm. Verify current product-page specifications before selection.
Geometry selects the motion system, while substrate behavior selects the process. Adhesion, static, heat sensitivity, surface energy, coating consistency, and white-ink opacity can overturn an otherwise sensible machine choice. Require tests on production blanks from the intended supplier because a visually similar bottle, board, or coating may behave differently under ink and curing.
On a flatbed, the production challenge is often planarity and repeatable Z height. Warped boards can alter head clearance. Small objects need nests that prevent movement and keep surfaces at a common height. Reflective, dark, or transparent pieces may require a white layer, while varnish changes both appearance and cycle structure. Confirm whether pins, vacuum zones, mechanical stops, or custom jigs suit the actual parts.
On a cylinder machine, concentric rotation matters. A straight bottle is simpler than a tapered tumbler, and a handle can restrict the available print arc or create a collision risk. Seams, lips, lids, and changing diameters affect where the image starts and ends. Ask the demo operator to show loading, datum selection, taper setup, seam control, and unloading rather than presenting only the finished item.
Compare the complete cost of serving the order book, not an isolated machine price. Capital equipment, options, fixtures, extraction or environmental needs, ink and maintenance consumables, operator handling, setup hours, sample development, and unusable output all belong in the model. Confirm every numeric input on a written quote or controlled production trial.
Build separate route costs for panels, nested flat pieces, straight cylinders, and tapered cylinders. For consumables, obtain the quoted ink configuration and use measured coverage from representative RIP files or trial jobs. Do not apply a generic ink cost per area to a layered white-and-varnish tumbler or assume a board mode represents a wrap job.
Labor deserves particular attention when one flatbed shares a rotary attachment. Record the observed minutes to clear the bed, mount and align the fixture, load the correct profile, print an accepted first piece, complete the round batch, remove the fixture, restore the flat setup, and approve the next panel. Multiply observed setup time by the forecast changeover schedule. This exposes lost hours without claiming that any fixed number of changeovers justifies another machine.
Implementation should turn the selected route into a controlled production cell. Before delivery, confirm footprint, access path, floor requirements, electrical service, ventilation or extraction guidance, temperature and humidity limits, network needs, ink storage, and safe material handling. Assign owners for site readiness, color workflow, fixture approval, operator training, and acceptance testing.
Fixtures are a production asset, not an afterthought. Ask who designs them, which file format or physical samples are required, how replacement fixtures are ordered, and how datum features prevent reversed or shifted loading. For nested flat parts, confirm spacing and collision clearance. For cylinders, confirm support points, grip method, taper accommodation, and change parts.
Training should cover daily startup and shutdown, nozzle checks, cleaning, ink handling, printhead clearance, profile selection, white and varnish workflows, fixture installation, recovery from interrupted jobs, and escalation. Have operators run both a normal job and a difficult representative SKU during acceptance.
A useful demo is designed to expose routing risk, not merely produce an attractive hero sample. Supply difficult artwork and production blanks, watch the complete setup, and inspect output under consistent lighting. Evaluate the first accepted piece, later pieces in the batch, and the transition between flat and round work when an attachment is proposed.
| Failure signal | Likely process concern | Demo check |
|---|---|---|
| A visible step or overlap at the wrap seam | Rotation, artwork length, or diameter setup | Use a registration pattern across the intended seam |
| Image drift around a tapered part | Taper compensation or part seating | Repeat the same artwork on several blanks |
| Banding or density change | Nozzle condition, pass mode, or cure interaction | Inspect solids and gradients across the image |
| White halo around color | Layer registration or artwork trapping | Use fine reversed type and colored edges over white |
| Poor adhesion at edges | Cleaning, treatment, ink, or cure mismatch | Apply the agreed adhesion protocol after curing |
| Inconsistent placement in a nest | Fixture datum or loading variation | Measure repeated features across every cavity |
| Head-strike evidence or scuffing | Height variation, warp, or unsafe clearance | Include normal tolerance extremes in the sample set |
Also time the workflow rather than only the print pass. For a rotary attachment, observe installation, calibration, first-piece approval, removal, and restoration of flat production. For a dedicated cylinder, observe part loading and recipe changes between two diameters. Document any manual adjustments that depend on one experienced operator.
These answers frame the four questions that most often determine a mixed-book purchase. They do not replace a sample test or written quotation, because SKU geometry and demand patterns vary by shop. Use them to structure internal routing rules, then validate the proposed process with the actual panels, promotional blanks, drinkware, files, and acceptance criteria.
Both become a serious option when flat and round orders are each recurring, their deadlines overlap, or rotary changeovers would regularly displace profitable flat work. Quantify that case using the forecast queue and observed setup hours. Separate machines also allow fixtures and recipes to remain ready, but require separate capital, space, maintenance, and training commitments.
Route boards and flat promotional items to a flatbed when their dimensions, thickness, and holding method fit the verified envelope. Route full-wrap drinkware and other round parts to controlled rotary production, especially when taper compensation or seam consistency is critical. Keep a written routing sheet for exceptions such as partial prints on unusually shaped objects.
An attachment can be enough when round work is occasional, batches can be scheduled together, the demonstrated geometry fits, and changeovers do not threaten panel commitments. A dedicated cylinder is more defensible when wraps are routine, tapers are important, or shared-machine transitions consume scarce hours. Base the comparison on observed workflows and a written quote.
A shop may begin with the platform serving its dominant revenue lane, while documenting the secondary lane for later expansion. Preserve sample files, recipes, diameter and size data, fixture drawings, and changeover records. Before adding equipment, repeat the order-book analysis and confirm that the proposed machine removes the measured constraint without creating an unsupported capability assumption.
The next step is a scoped application review built around real orders. Contact AndresJet with a compact SKU matrix and request both sample production and an itemized written quote. Ask the supplier to identify the recommended route for each part, required fixtures or options, verified specifications, implementation scope, and assumptions behind any throughput statement.
Use the AndresJet contact page and send each substrate, part size or cylinder diameter, printable length, monthly pieces or square meters, and required ink colors, including white or varnish. Include artwork and physical samples where possible. State the sample inspection method and defect-acceptance request, including seam, placement, adhesion, banding, color, and finish expectations. Ask for flatbed-only, cylinder-only, and combined configurations where relevant so the quote exposes changeover time, capacity allocation, fixtures, training, and support rather than assuming a machine choice in advance.

